 Контактор,автоматический выключатель,датчик,Кодер,ПЛК,Конвертер
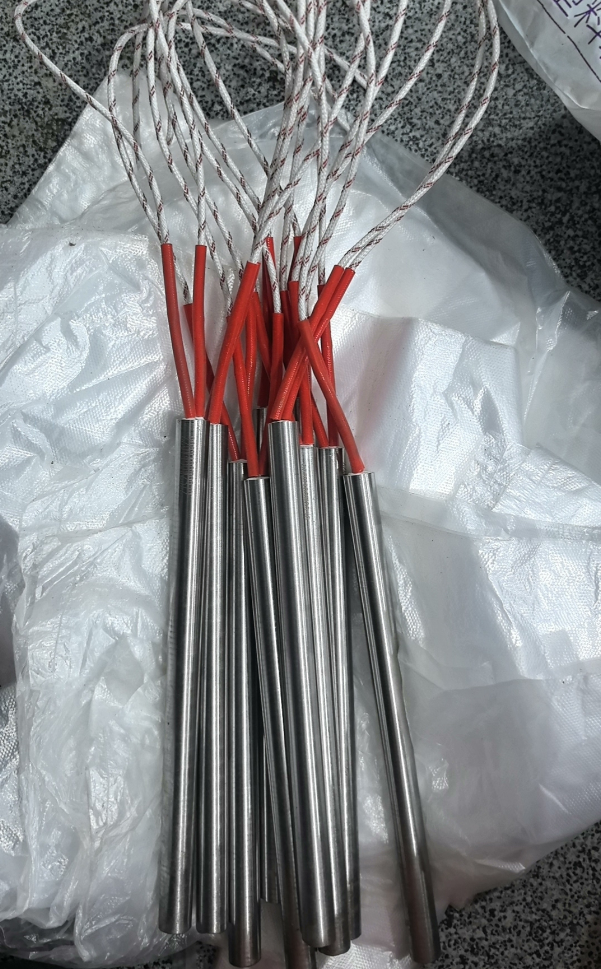
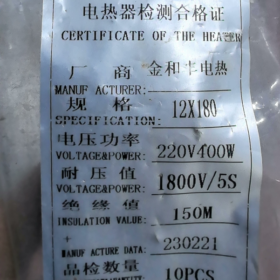
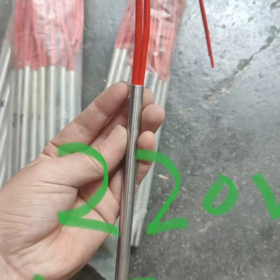
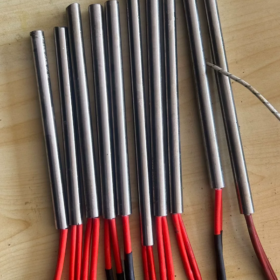
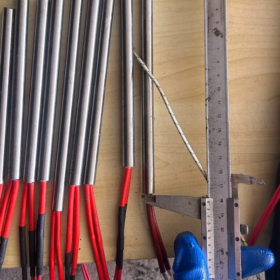
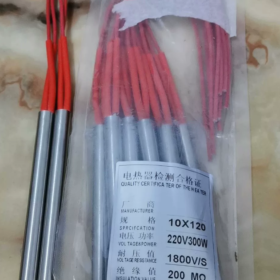
When ordering customized single-end cartridge heaters for molds, please provide all the following parameters in one go, so we can offer an accurate quotation.
- Mandatory Core Parameters
- Tube Diameter (Outer Diameter)
например: 6мм / 8мм / 10мм / 12мм / 16мм / 20мм, и т. д..
- Общая длина
Overall length including heating section + cold section (Единица: мм)
- Effective Heating Length
Length of the actual heating zone; the cold end does not generate heat.
- Рабочее напряжение
Common options: 220В / 380В / 110В / 24В / 36В
- Номинальная мощность
например: 300Вт / 500Вт / 800Вт / 1КВт / 2КВт, и т. д..
If power is unknown, provide: heating medium, целевая температура, and heating-up time for factory calculation.
- Lead Wire Type / Lead Wire Length
Прямой провод: silicone wire / Teflon wire, specify length
With terminal posts / распределительная коробка
Single-end wire outlet direction
- Sheath Material
Common options:
Нержавеющая сталь 304 (standard molds, ≤450℃)
Нержавеющая сталь 321 (medium-high temperature, ≤600℃)
Stainless Steel 310S (high-temperature molds, ≤800℃)
Incoloy (ultra-high temperature, устойчивый к коррозии)
- Common Custom Structural Parameters (Необязательный)
- With or Without Retaining Plate / Locating Plate
Provide diameter, thickness and position of the plate.
- With or Without Thread
например: М8 / М10 / М12 / M14 / M16 / М20
Provide thread length and position.
- Sealing Type
Ordinary adhesive sealing
High-temperature sealing
Waterproof / moisture-proof sealing
- Среда применения
Mold heating (plastic mold / die-casting mold)
Dry heating
Liquid heating
Temperature requirement: maximum operating temperature
- Tolerance Requirements
Diameter tolerance, length tolerance, and fitting requirements.
III. Optional Parameters for Extended Service Life
Internal heating wire material (NiCr 2080 / FeCrAl)
Magnesium oxide grade (стандартный / high-temperature high-density)
With or without tube reduction and annealing treatment
With or without thermocouple hole (can be built-in K-type thermocouple)
For mold applications, the simplest standard specification format is as follows:
> Single-end cartridge heater, diameter Φ10mm, total length 200mm, heating length 150mm, 220V 600W, 304 материал, 150mm silicone lead wire, with retaining plate.
Need me to generate a ready-to-send standard parameter text based on your mold dimensions?
Single-End Cartridge Heater (Single-End Heater / Cartridge Heater)
A single-end mold cartridge heater is a tubular electric heating element with wiring only at one end, mainly used for efficient heating in confined spaces or complex molds. It is widely applied in injection molding, литье под давлением, plastic molding and other industrial fields.
- Основная структура & Принцип работы
| Компонент | Материал & Функция |
| Metal Sheath | SS304 (≤500℃), SS321 (≤600℃), SS310S (≤800℃), provides mechanical protection and heat conduction |
| Нагревательный элемент | NiCr alloy (2080) or FeCrAl alloy wire, generates Joule heat when energized |
| Insulation Filling | High-purity magnesium oxide powder (density ≥2.8g/cm³), изоляция + high-efficiency heat transfer, compacted by tube reduction |
| Lead Wire | High-temperature resistant wire (силикон / Тефлон), single-end outlet for easy wiring and fixing |
Принцип работы: Electric current passes through the resistance wire to generate heat, which is transferred through magnesium oxide powder to the metal sheath and then to the mold, achieving precise temperature control.
- Ключевые особенности & Преимущества
- Маленький размер, high power density: Power per unit area up to 2.5–50W/cm², ideal for rapid heating
- High thermal efficiency (≥90%): Concentrated heating, fast thermal response, steep temperature rise curve
- Простая установка: Single-end wiring design, insertable into mold holes, adaptable to complex structures
- Высокая долговечность: Fully sealed structure, shockproof and corrosion-resistant, service life up to 5,000–10,000 hours
- Flexible customization: Customizable diameter, длина, власть, shape (U-type / threaded / flanged)
III. Specification Table
| Параметр | Общие характеристики | Примечания |
| Диаметр (Д) | Micro: 2–5 мм | Commonly 6mm, 8мм, 10мм, 12мм |
| Стандартный: 6–25mm | ||
| Imperial: 1/4″–1″ | ||
| Длина (л) | 20–2000mm | Настраиваемый, including heating and cold sections |
| Напряжение | 12В / 24В / 36В / 110В / 220В / 380В | 220V for small/medium equipment, 380V for large equipment |
| Власть | 50W–10kW | Calculated by surface load: W=π×D×L×w/cm² |
| Surface Load | Стандартный: 1–3W/cm² | 1–3W/cm² for plastic molds, 5–15W/cm² for metal molds |
| High-temperature: 3–6W/cm² | ||
| Особенный: 6–15W/cm² | ||
| Рабочая температура | SS304: ≤500℃ | Special materials available for over 1000℃ |
| SS321: ≤600℃ | ||
| SS310S: ≤800℃ |
- Приложения
- Plastic Molds: Инъекция / blow molding / extrusion molds, 200–400℃, improves molding quality
- Die-Casting Molds: Zinc / алюминий / magnesium alloy die-casting, requires rapid heating and high-temperature resistance
- Hot Runner Systems: Ensures uniform melt flow, increases production efficiency
- Другие отрасли: Медицинское оборудование, лабораторные инструменты, химические реакторы, sealing machinery, и т. д..
- Выбор & Power Calculation Guide
- Core Power Formula
- П = (M × cp × ΔT) / т + Qloss
М: Mold weight (кг)
cp: Specific heat of steel (≈470 J/kg·K)
ΔT: Temperature difference (℃)
т: Heating time (с)
Qloss: Heat loss (≈10–30% of total power)
- Surface Load Reference
| Heating Medium | Recommended Surface Load | Примечания |
| Dry heating in air | 0.5–1.5W/cm³ | Ensure sufficient heat dissipation |
| Liquid heating | 2–4W/cm³ | Flow rate affects heat dissipation |
| Metal molds | 5–15W/cm² | Higher when contact is excellent |
| Plastic molds | 1–3W/cm² | Avoid local overheating and deformation |
- Dimension Matching Rules
Fit between heater and mold hole: H7/g6 or H7/f7 for tight contact
Effective heating length must cover the heating zone; cold end extends outside for wiring
Reserve 0.1–0.2mm for thermal expansion to prevent jamming
- Установка & Обслуживание
Этапы установки
- Ensure verticality and smoothness of mold holes to avoid scratching the heater surface
- Clean holes and apply thermal grease / thermal adhesive to improve efficiency by 30–50%
- Insert gently, avoid heavy knocking
- Insulate wiring terminals properly, keep away from high-temperature areas
- Use with temperature controller, recommended fluctuation ±1℃
Обслуживание & Замена
- Operate only after cooling to room temperature to prevent burns
- Regularly clean carbon deposits / scale with fine sandpaper
- Inspect lead wire insulation, замените, если повреждено
- Replace heater if uneven heating or power drop occurs
VII. Общие проблемы & Решения
| Проблема | Причина | Решение |
| Перегорание нагревателя | Excess power density / плохой отвод тепла | Reduce surface load / improve heat transfer / increase cooling |
| Uneven heating | Плохой контакт / improper hole design | Reinstall with thermal grease / optimize hole layout |
| Electric leakage | MgO damp / повреждение изоляции | Replace heater / enhance sealing / избегайте влаги |
| Short service life | Frequent on/off / large temperature fluctuation | Optimize temperature control / use high-temperature materials |
Односторонние картриджные нагреватели являются предпочтительным решением для нагрева современных промышленных форм из-за их высокой удельной мощности., быстрый ответ и гибкая установка.
При выборе следует учитывать материал формы., целевая температура, время нагрева, точный расчет мощности и поверхностной нагрузки. Правильная установка и контроль температуры значительно повышают производительность и качество продукции..
Need me to calculate total required power, recommend diameter / длина / quantity and surface load based on your mold material, масса, target temperature and heating time? Just provide these parameters.


NH42-63-318x560.png "Автоматические переключатели резерва типа PC CHINT (АТС)НХ42-63/4СЗ")