 Контактор,автоматический выключатель,датчик,Кодер,ПЛК,Конвертер
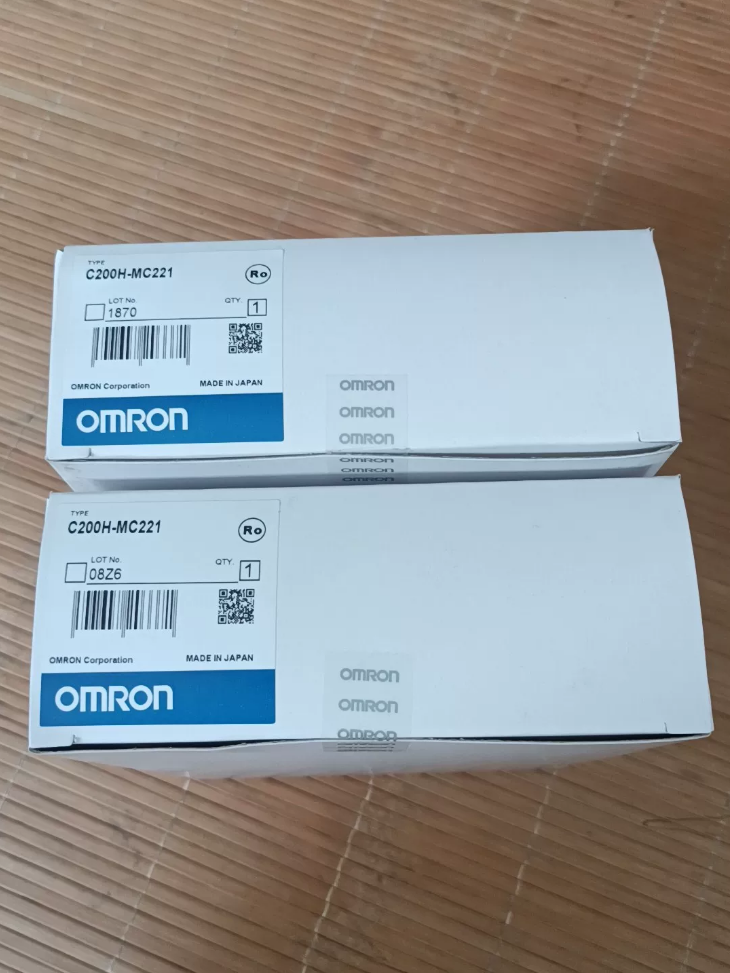
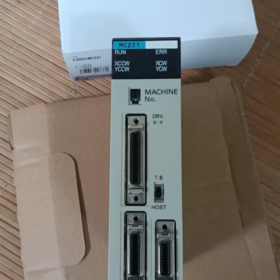
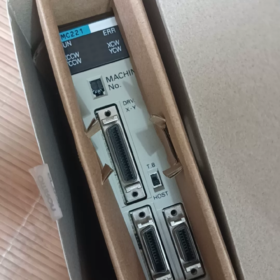
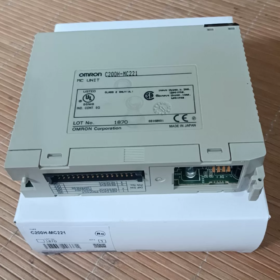
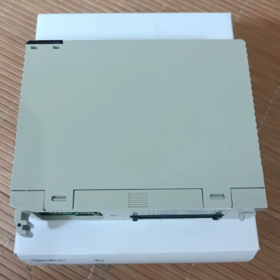
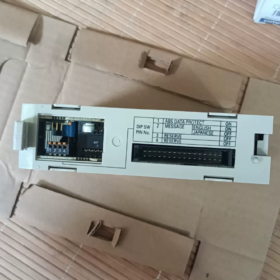
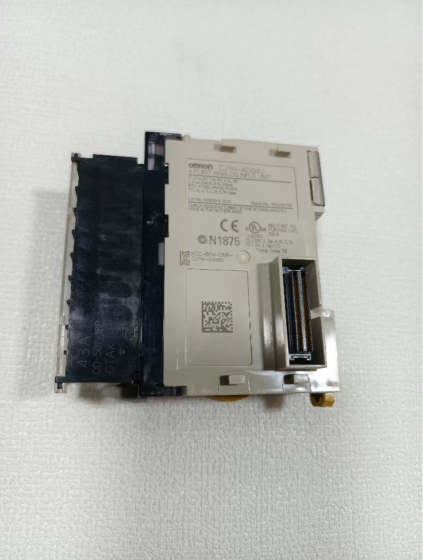
Полное название продукта: C200H Series 2-Axis Motion Control Unit
Статус: Discontinued in March 2017, order intake terminated. No brand-new factory stock available; only used or refurbished units circulate on the market.
PLC Backplane Compatibility: C200H / C200HS / C200HX/HG/HE racks
✅ Core Overview
The ОМРОН C200H-MC221 is an older-generation analog speed command 2-axis motion module. It adopts independent G-language (multi-task) programming and semi-closed-loop control. It outputs ±10 V analog voltage to servo drives (OMNUC W/U series analog servos) and supports linear and circular interpolation. It is widely applied to XY worktables, material transfer stations and simple cutting equipment.
Важное примечание: Analog output type, NOT pulse-output positioning module
📋 Key Technical Specifications
| Элемент | Технические характеристики |
| Number of Controlled Axes | 2 топоры (2-axis synchronized interpolation supported) |
| Режим управления | Semi-closed loop, analog speed command output (±10 V) |
| Интерфейс энкодера | Differential line receiver, maximum response frequency 250 кппс (×4 multiplication); supports incremental / absolute encoders (OMNUC W/U) |
| Interpolation Functions | Linear interpolation, planar circular interpolation, PTP point-to-point positioning, interrupt fixed-length feed |
| Ускорение / Deceleration | Trapezoidal / S-curve; время ускорения/торможения: 0~9998 ms (2 ms step) |
| Command Range | -39,999,999 ~ +39,999,999 |
| Minimum Command Unit | 1 / 0.1 / 0.01 / 0.001 / 0.0001; Единица: mm/inch/degree/pulse |
| Program Architecture | До 2 tasks; Single task: 100 programs, 800 blocks; Dual tasks: 50 programs and 400 blocks per task |
| Position Data Storage | Макс. 2000 position sets (single-axis operation) |
| M-Code Function | M-code 0~999 for auxiliary action output |
| Backplane Occupancy | 20 СН (занимает 2 rack slots) |
| Источник питания | DC5V: 0.65 А (Макс. 0.85 A with hand-held teaching box); 24 В постоянного тока: меньше, чем 0.2 А |
| Масса | <500 g |
| Дополнительные аксессуары | Hand-held teaching box CVM1-PRO01-V1, MPG handwheel, programming software CX-Motion Ver.2 |
🧩 System Composition
- Installed on the backplane of C200H-series CPU, independent of PLC ladder logic: G-language motion programs run inside the MC module, and the main PLC program only handles signal interaction.
- DRV Connector: 2-axis analog command + обратная связь энкодера
- I/O Connector: General-purpose I/O for external start/stop, hold, перезагрузить, external trigger and other signals
- Upper-computer Commissioning: Download G-code via CX-Motion software on PC; a dedicated hand-held teaching box can also be connected for manual operation and point teaching.
🔁 Replacement Options (Recommended by Original Manufacturer)
- Original Official Recommendation: CJ1W-NC213 (CJ-series 2-axis positioning module, тип импульса). Its hardware architecture is completely different. G-language programs cannot be directly migrated and must be fully rewritten.
- Legacy Transition Alternative: CS1W-MC221-V1 (same G-language motion architecture; discontinued in March 2025)
⚠️ Migration Challenges: The C200H-MC221 works with analog servos; the CJ1W-NC213 is designed for pulse-command servos. Servo drives must be replaced. Rewiring, control logic and programming system all require modification, resulting in heavy renovation workload.
🛠️ Inspection Checklist for Second-hand Spare Parts Procurement
- Visual Check: Oxidation of backplane gold fingers, вздутие конденсаторов, bent or corroded connector pins
- Тест при включении питания: Observe unit LED indicators (RUN/ERR); no faults or steady red light
- Static Continuity Test: No short circuit on DRV and I/O terminals
- Program Burn-in Test: Load simple G-language program to verify successful download without memory errors. If conditions permit, run point positioning with servo under no-load condition.
- Common Chronic Defect: Aging internal electrolytic capacitors of old modules. Long-term storage may cause crash after power-up, random position loss and unstable communication.
⚠️ Common Fault Phenomena
Steady red ERR light: DIP switch conflict of unit number, poor backplane contact, internal hardware damage of the module
Servo No Movement: Failed ±10 V analog output, broken encoder feedback cable
Position Drift / Потеря импульса: Interference on encoder cable, module aging, poor earthing
Failed G-program Download: Incompatible new CX-Motion version, damaged communication cable
📌 Software Environment
Программное обеспечение: CX-Motion Ver.2, integrated in CX-One; only compatible with legacy Windows (XP/Win7). Partial compatibility with Win10, poor compatibility with Win11. New CX-One releases no longer support project maintenance for this module.
HS Code Reference
8537101190 (Programmable controller motion control unit. Declare according to actual goods for import customs clearance of second-hand units)
C200H-MC221 Servo Drive Compatibility List
Основной принцип: C200H-MC221 outputs ±10 V analog speed command with semi-closed-loop control. The module directly reads differential encoder signals from the servo. Factory design originally matched OMNUC U / Вт / ЧАС / M series analog servos, all obsolete discontinued models.
✅ OMRON Servos Recommended by Manual (Native Support, Direct Connection via Dedicated DRV Cable)
- OMNUC U Series (R88D-UA□□) [Наиболее широко используемый]
Диапазон мощности: 30 W ~ 750 Вт, single-phase AC100/200 V
Model Examples: R88D-UA03L, R88D-UA08HA, R88D-UA20HA
Matched Motors: R88M-U series (supports incremental / absolute encoders)
Dedicated Cable: R88A-CPU00jM2
- OMNUC W Series (R88D-WT□□)
Legacy high-performance analog servo, such as R88D-WT01H / WT04H
Supports absolute encoder, compatible with SEN battery signal for MC221 absolute encoder
- OMNUC H Series (R88D-H□□)
Legacy H-series analog servo; dedicated cable R88A-CPH00jM2
- OMNUC M Series (R88D-M□□)
M-series analog servo; dedicated cable R88A-CPM00jM2
All above OMRON U/W/H/M servos are discontinued; only second-hand / dismantled spare parts available in the market.
✅ Third-party Servos [Compatible but not natively matched; rewiring required, no off-the-shelf dedicated cable]
All the following conditions must be satisfied to connect to C200H-MC221:
- The drive supports speed control mode with ±10 V analog voltage speed command input
- The encoder adopts differential line driver output (Line Driver, А/Б/З, incremental; partial models support ABS)
- Available signal terminals: servo alarm output, servo ON status, alarm reset signal (these handshake signals are required for MC module DRV port)
- Maximum encoder output frequency ≤250 kpps (upper limit of module front-end circuit)
Brand Examples: Yaskawa legacy SGDM (analog speed mode), Mitsubishi MR-J2S (analog speed), Panasonic MSDA/MSME old analog servo, и т. д..
⚠️ Критическое ограничение: The module cannot accept processed position pulse signals from servo drive. Encoder signals must be routed directly to C200H-MC221. Position cannot be forwarded to MC unit after closed-loop processing inside the drive. This is a common pitfall in retrofitting projects!
❌ Servos Not Directly Applicable
- Modern pulse-type servos (пульс & direction interface only, no ±10 V speed analog): R88D-KT/KN, МР-J4, SGDV pulse mode, и т. д..
- Fieldbus servos: EtherCAT, MECHATROLINK, RS485 fieldbus servos
- Encoder with open-collector output only (non-differential): prone to data loss in long-distance transmission
- Absolute encoder without SEN battery interface (SEN signal required for original U/W series ABS motors)
⚠️ Key Risks of Third-party Servo Retrofit
- Electronic gear ratio, unit and encoder resolution inside G-language program must be re-matched
- Custom wiring adapter required for DRV connector pin definition; no ready-made cable
- Analog zero drift, poor earthing and shielding defects will cause positioning drift
- Timing of servo ON, alarm and reset handshake must match MC221 logic; otherwise the MC module reports ERR
- High requirement on differential encoder signal quality; interference directly results in position loss
📌 Selection Advice
Maintain original machine with spare parts: Prefer R88D-UA (U series). It is the primary original matched model for MC221. Электропроводка, SEN absolute encoder and alarm handshake are fully compatible and ready to use with original cables.
New servo replacement solution: It is not recommended to retain C200H-MC221. Complete system upgrade (ПЛК + motion module + сервопривод) is suggested to avoid risks of discontinued spare parts.
Typical Application Cases of C200H-MC221 (Original Manual + Domestic Installed Legacy Equipment)
Core Capability: 2-axis synchronized linear/circular interpolation, independent G-language execution, ±10 V analog speed output, semi-closed loop. Suitable for XY 2-axis trajectory control of medium and small equipment. All cases are legacy projects on old machines; this unit is no longer selected for new machines.
Случай 1: XY Worktable / Planar Transfer Station (Самый распространенный)
Промышленность
Электронная сборка, PCB inspection, small material handling
Конфигурация системы
ПЛК: C200HX/C200HE
Motion Unit: C200H-MC221
Сервопривод: R88D-UA (OMNUC U series), X/Y two axes
Аксессуары: CVM1-PRO01-V1 hand-held teaching box
Процесс
- PLC handles logic for conveyor lines, air cylinders, sensors and safety circuits; all motion trajectories are stored in G-program inside MC221.
- Point Teaching: JOG movement and coordinate saving via hand-held box; до 2000 position sets can be stored.
- Action Flow: Home return → rapid movement to pick position → linear interpolation transfer → material release → return to standby position.
- M-code Interaction: When MC executes M-code, it notifies PLC to perform auxiliary actions such as clamping, air blowing and blanking.
Функции
Two axes can run point-to-point independently or perform linear synchronous motion; widely used for planar handling and product picking.
Болевые точки (Common Defects of Old Equipment)
Aging module electrolytic capacitors and analog zero drift cause positioning deviation after long-time operation; spare parts for U-series servos are difficult to source.
Случай 2: Simple 2-Axis Cutting Machine (Shaped Glass / Sheet Cutting, Classic Consulting Case)
Промышленность
Glass processing, acrylic sheet, thin plate cutting
Конфигурация системы
C200H-MC221 + R88D-WT analog servo
Процесс
G-language supports circular + linear interpolation, enabling machining of 2D contours (circles, polygons, special-shaped profiles).
Workflow: CAD drawing → convert to G-code → download to MC module via CX-Motion
Z-axis of cutting head is controlled separately by PLC (Z-axis not processed by MC221), while XY axes perform trajectory interpolation via MC.
Ограничения
Not a professional CNC; no tool radius compensation or advanced macro programs. Only suitable for simple 2D contour cutting, poor performance for complex curves. Many equipment manufacturers selected this solution in the past as an alternative to simple NC controllers.
Случай 3: Palletizing / Depalletizing (Planar Pallet Table)
Промышленность
Упаковка, grain, building material small-piece palletizing
Процесс
XY two axes move along matrix points on plane with PTP point-to-point control to place products row by row.
MC221 stores a complete palletizing point table. PLC only sends start signal, and MC automatically runs points in sequence.
Supports interrupt fixed-length feed; external photoelectric trigger can be used to start positioning once workpiece arrives.
Примечание: Only planar XY movement; 3D palletizing is not available. Z-axis lifting must be controlled separately by PLC.
Случай 4: Grinder / Machine Tool Worktable Retrofit (Electrical Refurbishment of Imported Legacy Machine Tools)
Промышленность
Precision grinder, thread grinder, small special-purpose machine tool renovation projects
Процесс
XY servo feed of worktable, cycles for rough grinding, finish grinding and wheel dressing; S-curve acceleration/deceleration is adopted to reduce impact and improve surface finish.
Home search, soft limit and hard limit are all processed inside the MC module.
PLC takes charge of hydraulic system, охлаждение, spindle start/stop and safety door interlock.
A large number of imported special machine tool retrofits in China in the late 1990s adopted this solution, and most of them have entered the spare parts maintenance period now.
Случай 5: Dispensing Machine & Coating Equipment
Промышленность
2D dispensing / trajectory coating for electronics and lighting products
Процесс
XY synchronized linear and circular interpolation for constant-speed coating along trajectory; M-code controls glue valve on/off.
Online speed override adjustment (0~199% interpolation override)
The hand-held box can modify trajectory points on site without downloading programs from PC every time.
Common System Architecture for All Cases
- Separation of Duties: PLC ladder diagram only handles I/O, безопасность, logic and communication; motion trajectory, interpolation and acceleration/deceleration are independently executed by C200H-MC221 via G-language, without occupying PLC computing resources.
- Signal Interaction: Through IR relay area, PLC sends start/stop/reset commands to MC; MC feeds back running status, positioning completion, M-code and alarm signals to PLC.
- Commissioning Method: Download G-program via CX-Motion Ver.2 on PC; hand-held teaching box for on-site JOG, home return and point teaching.
Выбор / Retrofit Tips (Важный)
✅ Suitable for: Simple 2D XY trajectory, point positioning, circular interpolation, spare parts maintenance of legacy equipment
❌ Не подходит для: New machine projects, multi-axis (>2 топоры), high-speed & high-precision applications, fieldbus servos, complex 3D trajectories
For major equipment overhaul, two options:
① Retain original system: Prepare only second-hand C200H-MC221+R88D-UA spare parts with high risks;
② Complete system retrofit: Replace with CJ2 + CJ1W-NC213 or modern fieldbus motion modules. G-language programs cannot be reused directly and need full rewriting.
Typical Fault Scenarios (High-frequency on-site Cases)
- Analog Drift: Deviation of cutting/dispensing trajectory, mostly caused by aging internal capacitors or poor earthing/shielding
- 0086 Servo Handshake Error: During third-party servo retrofit, servo ON and alarm timing mismatch MC221 logic
- Failed G-program Download: CX-Motion only supports XP/Win7; communication failure easily occurs on Win11
C200H-MC221 XY Dispensing Machine|I/O Allocation & Bill of Electrical Materials
System Overview: C200HX PLC + C200H-MC221 (2-axis G-language motion module) + OMRON R88D-UA analog servos for X/Y axes; Z-axis glue valve lifting controlled by standard PLC I/O; glue valve triggered by M-code.
MC221 occupies 20 СН. With default unit number 0, it occupies IR: IR200~IR219 (20 каналы), which is the core area for signal exchange between PLC and MC module.
- IR Address Allocation for PLC ↔ C200H-MC221 Communication (Unit No.0)
DIP switch of unit number set to 0, MC221 fixed occupying IR200~IR219; changing unit number will shift the starting address by 20 СН.
👉 PLC → MC221 (Выход, IR200~IR209, PLC writes, MC reads)
| Канал | Кусочек | Имя сигнала | Описание |
| IR200 | 0 | MC START | Trigger execution of selected G-program |
| IR200 | 1 | ПЕРЕЗАГРУЗИТЬ | Reset MC unit and clear alarms |
| IR200 | 2 | HOLD | Feed hold, axis pause |
| IR200 | 3 | ORG START | Start home return |
| IR200 | 4 | FEED OVERRIDE + | Increase override |
| IR200 | 5 | FEED OVERRIDE – | Decrease override |
| IR200 | 6 | PROGRAM SELECT bit0 | G-program number selection |
| IR200 | 7 | PROGRAM SELECT bit1 | G-program number selection |
| IR201 | 0~7 | PROGRAM SELECT bit2~bit9 | Select G-program number stored in MC (0~99) |
| IR202 | 0~15 | M-CODE ACK M-ACK | Acknowledge signal after PLC receives M-code |
| IR203~IR209 | – | Сдержанный | Available for variable writing and point parameter modification |
Logic Summary: MC executes G-language `Mxx` → M-code output to IR211, IR210.4 turns ON; PLC reads the M-code and triggers corresponding actions (например. M05 = glue valve open, M06 = glue valve closed). After completion of the action, PLC asserts the M-ACK handshake signal so that the MC can resume execution of the next trajectory segment.
- External I/O Allocation for Complete Machine (C200H Standard I/O Modules, C200H-ID/OD)
Rack: C200HX-CPU44, Источник питания: C200H-PS221
Цифровой вход (ID212, DC24V Input)
| Адрес | Сигнал | Примечания |
| 0 | System Start Pushbutton | Panel start |
| 1 | System Stop Pushbutton | Normal stop (not emergency stop) |
| 2 | Emergency Stop Signal (Северная Каролина) | Схема безопасности, wired in series with safety gate |
| 3 | Ворота безопасности | Guard gate; motion inhibited when gate open |
| 4 | Workpiece-in Photoelectric Sensor | Trigger upon workpiece arrival |
| 5 | Z-axis Upper Limit Sensor | Z glue valve upper position limit |
| 6 | Z-axis Lower Limit Sensor | Z glue valve lower position limit |
| 7 | X Positive Hard Limit | X-axis positive hard limit |
| 8 | X Negative Hard Limit | X-axis negative hard limit |
| 9 | Y Positive Hard Limit | Y-axis positive hard limit |
| 10 | Y Negative Hard Limit | Y-axis negative hard limit |
| 11 | X Home Proximity Sensor | X-axis home position |
| 12 | Y Home Proximity Sensor | Y-axis home position |
Цифровой выход (OD212, DC24V Output)
| Адрес | Сигнал | Примечания |
| 1000 | Z Solenoid Valve Retract Down | Glue valve descent |
| 1001 | Z Solenoid Valve Lift Up | Glue valve retraction |
| 1002 | Glue Valve Solenoid Valve | Glue discharge control (interlocked with M-code) |
| 1003 | Alarm Indicator Lamp | Fault lamp |
| 1004 | Run Indicator Lamp | Operating lamp |
| 1005 | Buzzer | Fault audible alarm |
| 1006 | Global Servo Enable Output | Common Servo ON signal for X/Y axes |
| 1007 | Запасной | Reserved for future use |
III. Bill of Electrical Materials
| Категория | Модель | Кол-во | Примечания |
| PLC CPU Unit | C200HX-CPU44 | 1 | C200H-series CPU |
| Блок питания | C200H-PS221 | 1 | Rack power supply |
| Motion Control Unit | C200H-MC221 | 1 | 2-axis analog motion, занимает 2 слоты |
| Входной модуль | C200H-ID212 | 1 | 16-point DC24V input |
| Модуль вывода | C200H-OD212 | 1 | 16-point DC24V output |
| X-axis Servo Drive | R88D-UA08HA | 1 | 750Вт, analog speed command |
| X-axis Servo Motor | R88M-UA08030H | 1 | With incremental encoder |
| Y-axis Servo Drive | R88D-UA04HA | 1 | 400Вт |
| Y-axis Servo Motor | R88M-UA04030H | 1 | With incremental encoder |
| MC Servo Cable X | R88A-CPU003M2 | 1 | Direct connection between MC221 DRV port and servo |
| MC Servo Cable Y | R88A-CPU003M2 | 1 | |
| Hand-held Teaching Box | CVM1-PRO01-V1 | 1 | JOG, home search, point teaching |
| Импульсный источник питания | 24 В постоянного тока 5 А | 1 | Power supply for I/O and sensors |
| Relay Module | DC24V Relay | По мере необходимости | Isolation drive for solenoid valves and indicators |
| МКБ | Single-phase AC220V | 2 | Separate circuits for control circuit and servo circuit |
| EMI Filter | Power EMI Filter | 2 |
NH42-63-318x560.png "Автоматические переключатели резерва типа PC CHINT (АТС)НХ42-63/4СЗ")