 Schütz,Leistungsschalter,Sensor,Encoder,SPS,Konverter
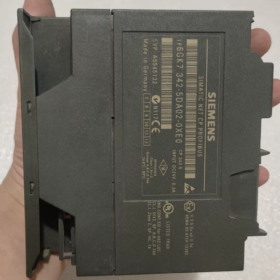
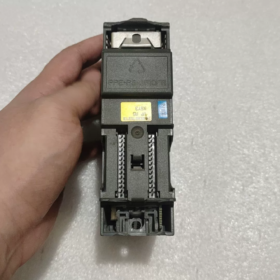
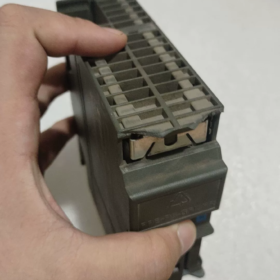
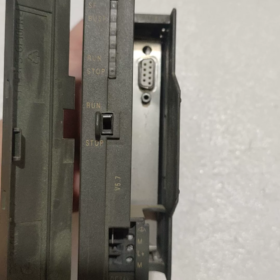
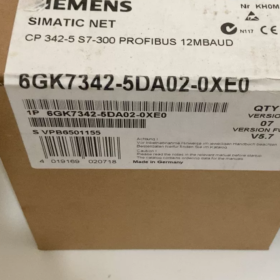
✅ Model Code Explanation
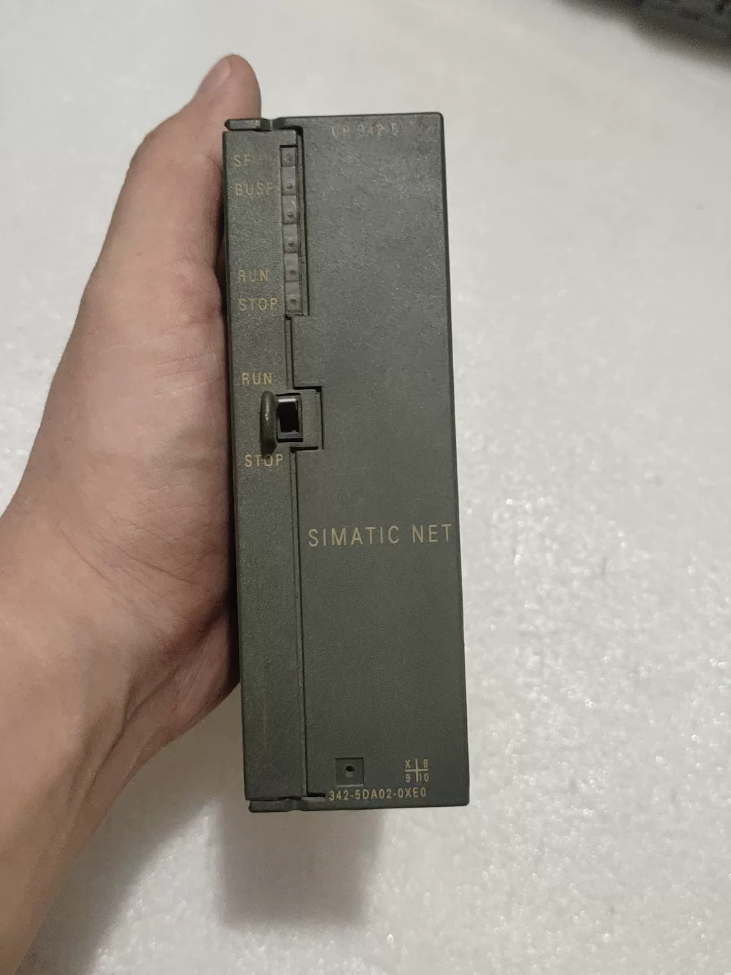
6GK7: SIMATIC Communications Processor (CP) Serie
342: PROFIBUS DP communications module for S7-300 platform
5: PROFIBUS DP interface
DA02: Version 2; 0XE0: product revision suffix
Full designation: CP 342-5 PROFIBUS DP Communications Processor, backplane bus module dedicated to S7-300 PLC
✅ Basic Overview
Status: Auslaufmodell (phase-out effective 2021-03-01). Original replacement part: 6GK7342-5DA03-0XE0
Designed to expand PROFIBUS DP interface for S7-300 PLC. It can operate as either DP Master or DP Slave. The independent communications processor offloads CPU communication workload.
✅ Core Functions
- PROFIBUS-DP: DP-Master / DP Slave (select one mode)
- Communication protocols: S7 communication, PG/OP programming & diagnostic communication, S5 protocol compatible
- Supports S7 routing, enabling cross-subnet PLC access
- Connects to S7-300 rack via backplane bus; RS485 PROFIBUS interface (9-pin female DB connector)
- Master mode: unterstützt bis zu 124 DP slaves; maximum I/O data: 244 Byte-Eingabe + 244 Bytes ausgegeben
- Slave mode: works as DP slave of S7-300 and connects to upper-level DP master
- Firmware V4.0 and above support DPV1 for diagnostics and PDM device parameter reading
✅ Electrical & Umweltspezifikationen
Stromversorgung: 5V DC from backplane bus; external 24V DC module supply
Stromverbrauch: ca. 2.5W
Betriebstemperatur: 0℃ ~ +60℃ (rack mounting)
Schutzklasse: IP20, DIN rail mounting for S7-300 rack
Baudrate: 9.6kbit/s ~ 12Mbit/s, standard PROFIBUS rates
Konfigurationssoftware: STEP7 V5.x (HW Config). Standard FC1(DP_SEND) and FC2(DP_RCV) must be called to read/write DP data
✅ Configuration Notes
CP342-5 does not map directly to process image area. FC1 and FC2 must be called in OB1 to exchange data between CPU and CP. This is a major difference from CPUs with integrated DP port (z.B., 315-2PN/DP).
FC1: DP_SEND, send data to DP bus
FC2: DP_RCV, receive data from DP bus
✅ Replacement & Spare Parts Information
- Original replacement: 6GK7342-5DA03-0XE0. Identical mechanical form factor for direct rack replacement. Hardware configuration must be updated to the new model and recompiled/downloaded; user program generally remains unchanged.
- Market status: DA02 is only available as used / dismantled spare parts. Inspection checklist: backplane contacts, DP connector, no corrosion, firmware version, DIAG lamp status upon power-up.
- Altenative for new projects (S7-300 not recommended): S7-1500 + CM1542-5
✅ Troubleshooting Guidelines (Second-hand Module Inspection)
PWR LED: steady ON = power normal
DIAG LED: rot = Fehler (bus short circuit, configuration error, firmware abnormality)
BUSF LED: DP bus fault; check terminating resistors, Verdrahtung, baud rate mismatch
Test procedure: power on without field bus load, download CP configuration individually in HW Config to eliminate backplane bus issues; short DP bus for communication test
✅ HS Code Reference
85176210 (programmable industrial communications processor, fieldbus communication module. For export customs declaration only; subject to local customs rulings.)
Siemens 6GK7342-5DA02-0XE0 (CP342-5) Anwendbare Branchen
Core positioning: PROFIBUS DP communications processor for S7-300, used to expand DP bus interface. For spare parts maintenance of legacy projects only; not recommended for new builds. Widely deployed in discrete and process industries with traditional PROFIBUS architecture.
http://Communications 🏭 Main Industry List
- Automobilbau (Most Typical)
Welding lines, Beschichtungsanlagen, final assembly conveyor lines, Roboterarbeitsplätze. CP342-5 acts as DP Master to connect robots, Frequenzumrichter, remote ET200 slaves and valve islands. A large number of older production lines still rely on this module for fieldbus control.
- Metallurgie
Hot/cold rolling, continuous casting and non-ferrous metal smelting. Heavy use of variable frequency drives and strong electromagnetic interference on site. Deterministic PROFIBUS DP communication suits roller tables, hydraulic and cooling system control.
- Zement & Baustoffe
Cement kilns, raw material conveying, packaging lines and crushing systems. Kiln outlet and mill areas are equipped with numerous DP instruments and drives; legacy lines commonly adopt S7-300 + CP342-5 architecture.
- Chemisch / Pharmazeutisch
Chemiefabriken, wastewater treatment and pharmaceutical production lines. Can operate as DP slave to connect to DCS, interfacing flow meters, pressure transmitters and valve positioners. Widely used for S7-300 stations inside explosion-proof cabinets.
- Energiewirtschaft
Auxiliary boiler controls, coal handling systems in power plants, wastewater treatment plants and pump stations. Used for DP bus acquisition and control of remote field I/O, valves and motors.
- Schienenverkehr
Tunnel ventilation fans, station HVAC and depot maintenance equipment. Traditional station automation extensively uses PROFIBUS DP.
- Logistik & Lagerung
Automated warehouse stackers and sorting conveyors. Connects encoders, Wechselrichter, photoelectric sensors and remote I/O.
- Allgemeine Maschinen
Große Werkzeugmaschinen (SINUMERIK paired with S7-300), Verpackungsmaschinen, Gummi & plastic extruders, papermaking equipment.
✅ Application Characteristics (Reasons for Industry Adoption)
- PROFIBUS DP bus with high real-time performance, suitable for multi-drive and distributed I/O networking; master supports up to 124 DP slaves
- Independent communications processor, offloads CPU communication load. Bus communication will not slow down PLC logic scan cycle
- Dual-mode DP Master/Slave: can serve as bus master or slave connected to upper DP master/DCS
- Supports S7 routing and PG/OP online debugging, convenient for cross-subnet program upload/download and online diagnostics
- Industrial wide temperature range 0~60℃ for workshop environment (IP20, must be installed inside control cabinet)
⚠️ Industry Usage Reminders
6GK7342-5DA02-0XE0 is discontinued, only for maintenance replacement of legacy equipment. New projects prefer PROFINET solutions
User program must call FC1 (DP_SEND)/FC2 (DP_RCV). Unlike CPUs with native DP port which directly map process image, this is the most common engineering pitfall
For high EMI environments (Metallurgie, medium frequency furnaces), use PROFIBUS shielded cable + terminating resistors. Fiber optic CP342-5 FO can be selected when necessary.
Siemens 6GK7342-5DA02-0XE0 (CP342-5) Application Cases in Automotive Manufacturing
Positionierung: Legacy PROFIBUS DP communications processor for welding & Montagelinien. Mass deployed in OEM plants commissioned between 2000~2015. No longer adopted for new lines; only spare parts maintenance for existing production lines.
Core feature: S7-300 CPUs without built-in DP port use CP342-5 to extend DP bus. FC1(DP_SEND)/FC2(DP_RCV) must be called for data exchange between CPU and CP; direct process image mapping is not available.
Fall 1: Body Welding Main Line at Passenger Vehicle OEM (Classic Case)
Projektübersicht
Body welding workshop of a domestic automaker. S7-300 CPU314 (no integrated DP port) + 6GK7342-5DA02-0XE0 as DP Master to control BIW assembly welding stations.
Hardware Architecture
S7-300 CPU314 + CP342-5 (6GK7342-5DA02-0XE0)
PROFIBUS DP bus: 1.5Mbit/s
DP slave list: ET200M distributed I/O, robot cabinet DP interface, servo positioning modules, pneumatic valve islands, welding controllers, safety relays
Bus nodes: 28 DP slaves
Funktionen
- CP342-5 operates as DP Master to cyclically send welding start/stop, clamp open/close and servo positioning commands. Reads clamp position feedback, robot status, welding current and fault alarms.
- Independent communications processor offloads CPU load; high-frequency robot interaction does not impact PLC logic scan.
- PG/OP routing supported, allowing engineers to monitor S7-300 program online from any bus node.
- Production data uploaded to workshop WinCC SCADA.
Engineering Pain Points
Severe electromagnetic interference in welding workshop from spot welding high current. Early projects often had flickering BUSF LED and intermittent slave drop-out. Mitigation: PROFIBUS shielded cable, terminating resistors at both bus ends, separate trunking for power and bus cables.
FC1/FC2 must be cyclically called in OB1. Omitting the function blocks results in normal bus configuration status yet zero data exchange.
Fall 2: Friction Conveyor for Body Transfer in Automotive Final Assembly
Projektübersicht
Passenger vehicle final assembly workshop. Multiple S7-300 sub-stations. CP342-5 configured as DP Slave for some stations, connecting to the overall DP Master (S7-400) of the conveyor line.
Hardware Architecture
Local S7-300 (CPU315) + CP342-5 (6GK7342-5DA02-0XE0), DP Slave mode
Upper-level Master: S7-400 CPU with integrated DP port
DP slave devices: Frequenzumrichter, Encoder, ET200S, station HMI
Funktionen
Each conveyor segment S7-300 independently controls friction drive motors, body positioning stops and stoppers. As DP Slave, CP342-5 uploads body barcode, position and fault status to upper master, and receives production scheduling commands.
Multiple conveyor segments linked to realize body queue scheduling across the whole assembly line.
Wartungshinweise
DA02 is an older revision. Long-term exposure to workshop temperature and humidity variation causes oxidation of DB9 DP connectors, triggering intermittent communication interruptions. This is a frequent failure point on legacy assembly lines.
Fall 3: Engine Cylinder Block Machining Line (Automotive Powertrain)
Projektübersicht
Weichai Deutz cylinder block production line. 4 sets of S7-300 systems, each equipped with one 6GK7342-5DA02-0XE0 as DP Master, controlling machine auxiliary equipment, conveyor rollers and inspection units. Central monitoring via WinCC.
Hardware Architecture
S7-300 CPU + CP342-5 DA02
DP slaves: ET200M remote I/O, Frequenzumrichter, workpiece identification sensors, 840D CNC DP interface
Bus baud rate: 1.5Mbit/s
Funktionen
CP342-5 handles DP bus data exchange to link CNC lathes and conveyors. Workpiece in-position signals, tool status and finished part inspection data are transmitted via DP to PLC, then uploaded to WinCC for production statistics and equipment OEE collection.
Classic case documented in public technical literature; many auto component factories adopt similar solutions.
✅ Historical Reasons for Selecting CP342-5 DA02 in Automotive Industry
- Early S7-300 CPUs such as CPU314 did not have integrated PROFIBUS DP interface, requiring external CP342-5 for DP bus expansion.
- Dedicated communication chip handles communication tasks independently without consuming CPU scan resources, suitable for high real-time welding stations with robots and multiple servos.
- DPV1 diagnostics supported to retrieve detailed slave fault information, enabling fast troubleshooting for automotive lines with high downtime costs.
- Dual Master/Slave mode supports segmented line networking and flexible distributed production line construction.
⚠️ Operation & Retrofit Notes for Automotive Production Lines
- 6GK7342-5DA02-0XE0 discontinued in 2021. Nur verwendet / dismantled spares available for line maintenance. Original replacement: 6GK7342-5DA03-0XE0. Same mechanical footprint, but hardware configuration must be updated and downloaded.
- Production line upgrade: new automotive plants fully adopt PROFINET and S7-1500 architecture, Profibus + CP342-5 is no longer used.
- High-incidence faults: BUSF alarm, DB9 connector issues, shield grounding and terminating resistors are top failure causes under welding workshop EMI. Red DIAG LED indicates configuration error or firmware mismatch.
- Programming pitfalls: CP342-5 does not use automatic I/O mapping. Incorrect FC1/FC2 data length triggers 8180 communication error, a common issue in multi-slave automotive projects.
NH42-63-318x560.png "Automatische Transferschalter vom Typ CHINT PC (ATS)NH42-63/4SZ")